Reliability, Verification & Maintainability
Proving and keeping the treadle lathe working: an FMEA that scores six failure modes by severity, occurrence, and detection (dust in the bearings, loosening wedges, and a loose crank pin rank highest) and ties each to a design answer; verification tests with numbers (flywheel coast-down, spindle speed, runout, center alignment in two seasons); availability from MTBF and MTTR; and a maintenance checklist by session, month, and season.
- 5 min
- 5 steps
- 3 questions
- Lesson 48 of 78
In this lesson
- Design from failure backward
- Verify with numbers
- Availability and repair
- Make maintenance a design input
- What to take from this
Picking up where you left off.
Design from failure backward
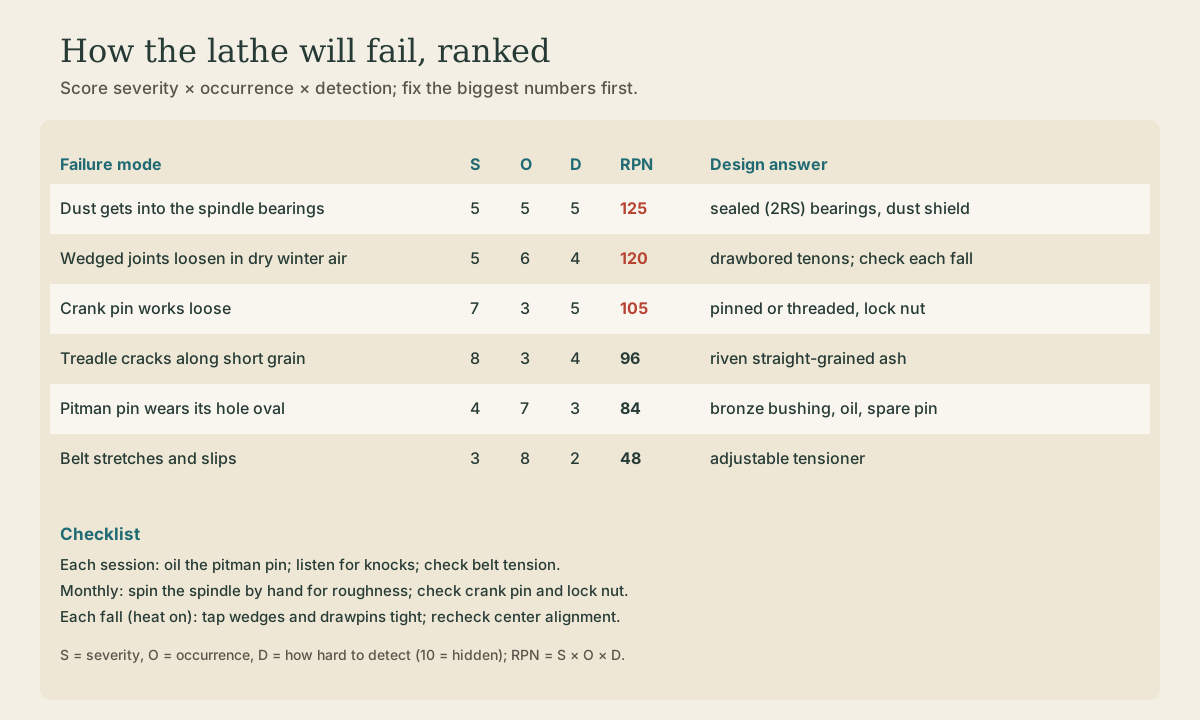
A machine is reliable when its likely failures have been found and designed out before it’s built. The tool for that is an FMEA (failure mode and effects analysis): list how each part could fail, what happens, and score three things from 1 to 10:
- Severity (S): how bad the effect is.
- Occurrence (O): how likely it is.
- Detection (D): how hard it is to notice before it causes harm (10 means hidden).
Their product, the risk priority number (RPN = S × O × D), ranks what to fix first. For the treadle lathe:
| Failure mode | S | O | D | RPN | Design answer |
|---|---|---|---|---|---|
| Dust gets into the spindle bearings | 5 | 5 | 5 | 125 | sealed (2RS) bearings, a dust shield |
| Wedged joints loosen in dry winter air | 5 | 6 | 4 | 120 | drawbored tenons; check each fall |
| Crank pin works loose | 7 | 3 | 5 | 105 | pinned or threaded with a lock nut |
| Treadle cracks along short grain | 8 | 3 | 4 | 96 | riven, straight-grained ash |
| Pitman pin wears its hole oval | 4 | 7 | 3 | 84 | bronze bushing, oil, a spare pin |
| Belt stretches and slips | 3 | 8 | 2 | 48 | an adjustable tensioner |
The scores are judgment, which is fine: the value is in being forced to think about each part. Notice what the earlier lessons already did: lesson 2 found that bearing fatigue isn’t the risk and dust is 1; lesson 3 found that fatigue from knots and grain slope, not static strength, governs the treadle 2; lesson 4 found the seasonal movement that loosens joints. The FMEA collects those into one list.
Quick check
5 × 5 × 5 = 125 against 8 × 3 × 4 = 96; both get a design answer.
Verify with numbers
Each requirement from the first lesson gets a test you can pass or fail:
- Foot stroke: measure the foot pad’s travel. Target about 9 inches.
- Flywheel: bring it to 100 rpm, stop treadling, and time the coast-down. Then make a heavy cut and count rpm before and during it. Target: no stall at the dead points, speed dip under about 10 percent.
- Spindle speed: count spindle revolutions in 15 seconds with a chalk mark, on each step of the pulley. Targets about 730, 550, and 440 rpm.
- Runout: a dial indicator on the faceplate face and on the spindle nose while turning by hand. Target: under a few hundredths of a millimeter at the nose.
- Center alignment: bring the centers together and check height with a straightedge, or turn a test cylinder and measure both ends. Target 0.5 mm. Repeat in winter and in summer, because lesson 4’s seasonal term only shows up then.
- Bearings: turn the spindle by hand. It should spin smoothly with no roughness or play.
MIT’s machine design course treats this as the second half of design: characterize the device you built against the requirements you set 3.
Playback is optional. If the player is unavailable, open the video at its source.
Quick check
Each requirement gets a test with a number.
Availability and repair
How much of the time the lathe is ready to use depends on how often it fails and how long a fix takes. With mean time between failures (MTBF) and mean time to repair (MTTR), availability A = MTBF ÷ (MTBF + MTTR). A machine that fails every 500 hours of use and takes 5 hours to fix is available 500 ÷ 505 ≈ 99.0 percent of the time; cut the repair to 1 hour and it’s 99.8 percent, without changing how often it fails.
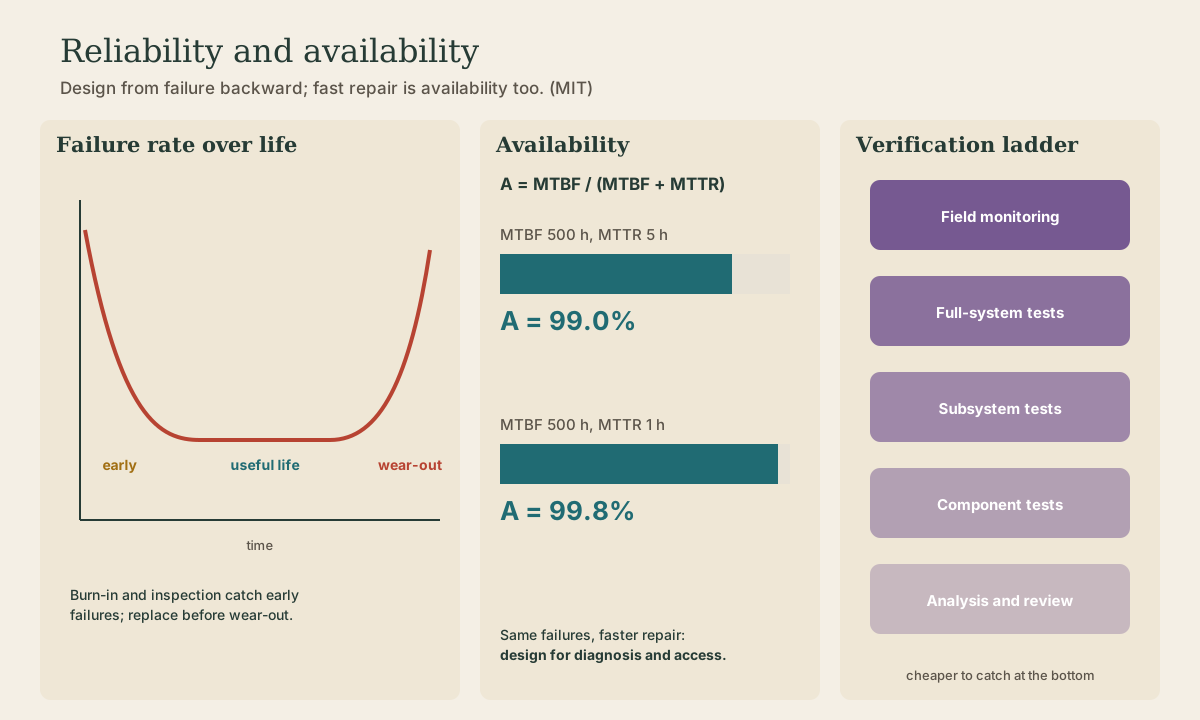
For the treadle lathe, that means: keep a spare pitman pin and bushing, a spare belt, and a pair of bearings on the shelf; make the pitman pin removable without taking the treadle off; and keep the shim stack for the tailstock labeled. A worn part that takes ten minutes to swap barely counts as a failure.
Quick check
A = MTBF ÷ (MTBF + MTTR). A spare pitman pin and bushing on the shelf is availability.
Make maintenance a design input
Write the maintenance down and build it into the machine:
- Each session: oil the pitman pin; listen for knocks; check belt tension.
- Monthly: spin the spindle by hand for roughness; check the crank pin and its lock nut.
- Each fall, when the heat goes on: tap the wedges and drawpins tight; recheck center alignment.
Then design so those jobs are easy: an oil cup on the pitman bushing, a wrench-sized flat on every nut, wedges you can reach with a mallet. Maintenance that’s hard to do doesn’t get done.
What to take from this
Find the failures before they happen: an FMEA scores severity, occurrence, and detection, and the top RPNs here (bearing dust, loosening wedges, a loose crank pin) each get a design answer. Verify every requirement with a number, and check center alignment in both seasons. Availability is MTBF ÷ (MTBF + MTTR), so spares and quick-change parts count as much as durability. Build the maintenance checklist into the design.
Lesson complete
Nice work.
Sources for this lesson
- 1Dynamic Load Ratings and Fatigue Life (ABCs of Bearings). NSK. verifiedBasic rating life L10 is the number of revolutions (or hours) that 90 percent of identical bearings reach before rolling-fatigue flaking; the basic dynamic load rating C is the constant load giving an L10 of one million revolutions. For ball bearings L10 = (C/P)^3 million revolutions, so doubling the load cuts life to one eighth. Bearing life in practice also ends from noise, vibration, torque, or temperature.
- 2Wood Handbook, Chapter 5: Mechanical Properties of Wood. USDA Forest Service, Forest Products Laboratory. 2021. verifiedTable 5-3a, clear wood at 12% MC: white ash SG 0.60, MOR 106 MPa, MOE 12.0 GPa, work to maximum load 115 kJ/m3; sugar maple 0.63, 109 MPa, 12.6 GPa, 114; white oak 0.68, 105 MPa, 12.3 GPa, 102.
- 3Elements of Mechanical Design. MIT OpenCourseWare. verifiedModeling, design, integration, fabrication, and characterization of bearings, springs, gears, cams, mechanisms, shafts, drives, and connections.