Datums, Fits, Tolerances & Error Budgets
Keeping the treadle lathe's headstock and tailstock centers in line: picking the bed as the datum, a signed tolerance stack for center height (worst case 0.8 mm against a 0.5 mm requirement; root-sum-square 0.37 mm), the seasonal term from wood movement (2.1 mm flatsawn versus 1.1 mm quartersawn for a 100 mm oak block from 6 to 12 percent moisture, about 1 mm of mismatch if the blocks differ), making it common-mode or turning the grain, designing in a shim instead of a tight tolerance, and bearing fits: tight where the ring rotates relative to the load, loose where it doesn't, and never pressed straight into wood.
- 5 min
- 6 steps
- 3 questions
- Lesson 46 of 78
In this lesson
- The requirement
- Pick the datum
- Build a signed stack
- The seasonal term
- Bearing fits
- What to take from this
Picking up where you left off.
The requirement
When you turn a chair spindle between centers, the drive center in the headstock and the dead center in the tailstock define the axis. If one is higher than the other, the work turns on a tilted axis, and the tailstock end wobbles and pulls. Write the requirement as a number: the two centers within 0.5 mm of the same height, in every season.
Pick the datum
Everything is measured from one reference: the top of the bed ways, the surface both the headstock and tailstock sit on. That’s datum A. The front edge of the ways, which keeps the tailstock lined up sideways, is datum B. Every height that matters (each block, each bearing housing, each center) is dimensioned from A, so errors add up along one chain instead of several.
Build a signed stack
Trace the center height from the datum up through each part, on both ends, and give each link a tolerance:
| Link | Tolerance (± mm) |
|---|---|
| Bed flatness between headstock and tailstock | 0.2 |
| Headstock block thickness (planed) | 0.2 |
| Bearing housing center height | 0.1 |
| Tailstock block thickness (planed) | 0.2 |
| Tailstock center height in its barrel | 0.1 |
Worst case, every link at its limit in the bad direction: 0.2 + 0.2 + 0.1 + 0.2 + 0.1 = 0.8 mm, over the 0.5 mm requirement. Root-sum-square, which assumes independent random errors that rarely all line up: √(0.2² + 0.2² + 0.1² + 0.2² + 0.1²) = √0.14 ≈ 0.37 mm, inside it. RSS is a fair bet for production runs; for one lathe, you’ll get whatever the actual parts are.
So don’t tighten every tolerance. Design in an adjustment: a pair of thin shims under the tailstock, chosen at assembly by turning a test piece and measuring. One adjustable link replaces precision everywhere else. Control the few dimensions that reach the function, and leave the rest loose.
Quick check
Adjustment at assembly is cheaper than tolerance on every part.
The seasonal term
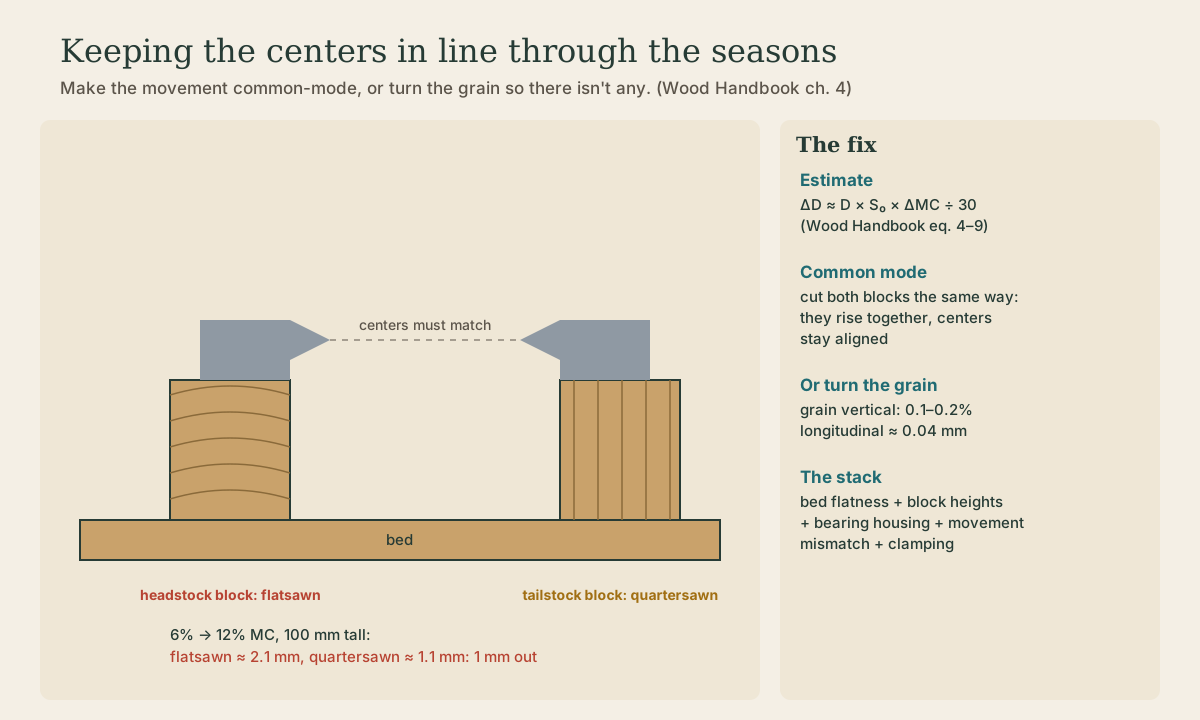
The stack above is for a lathe built and checked on one day. Wood adds a term that changes with the weather. Below the fiber saturation point, a piece’s width changes roughly in proportion to its moisture change: ΔD ≈ D × S₀ × ΔMC ÷ 30, using the tangential shrinkage S₀ for flatsawn width and the radial value for quartersawn 1.
Say the centers sit on white oak blocks 100 mm tall with the grain running horizontally, and the shop goes from about 6 percent moisture in a heated winter to 12 percent in a humid summer (ΔMC = 6):
- Flatsawn (height across the rings, tangential 10.5 percent): 100 × 0.105 × 6 ÷ 30 ≈ 2.1 mm.
- Quartersawn (radial 5.6 percent): ≈ 1.1 mm 1.
That’s more than the whole tolerance budget. But look at what actually matters: the difference between the two ends. Two ways out:
- Make it common-mode. Cut both blocks from the same board, oriented the same way. They grow together, and the centers rise together and stay aligned. Cut one flatsawn and one quartersawn, and they drift about 1 mm apart every summer.
- Turn the grain. Orient the blocks with the grain running vertically. Longitudinal shrinkage is only 0.1 to 0.2 percent green to ovendry 1, so the same moisture change moves a 100 mm block about 0.04 mm.
Quick check
Cut both the same way so they move together, or run the grain vertically.
Bearing fits
The spindle bearings bring in a different kind of tolerance: how tight each ring fits its seat. The rule is about which ring turns relative to the load 2:
- The belt pulls the spindle one way while the spindle, and the inner ring with it, turns. The inner ring sees a rotating load, so it needs a tight fit on the shaft. With too little interference it creeps, slipping around and wearing the seat 2.
- The outer ring is stationary relative to the load, so it can take a looser fit in the housing 2.
- Too much interference can crack a ring 2, so use the maker’s recommended shaft and housing tolerances.
One more rule for a wooden machine: don’t press a bearing straight into wood. The hole will grow and shrink with the seasons, loosening in summer and pinching in winter. Mount the bearings in cast or steel housings (pillow blocks or flanged units) bolted to the wood, and let the bolts and slots take the movement.
Playback is optional. If the player is unavailable, open the video at its source.
Quick check
A loosely fitted rotating ring creeps around its seat and wears it.
What to take from this
Write alignment as a number (centers within 0.5 mm), pick the bed top as datum, and trace a signed stack: worst case 0.8 mm, RSS 0.37 mm. Add a shim at assembly instead of tightening everything. Wood adds a seasonal term: about 2.1 mm flatsawn versus 1.1 mm quartersawn for a 100 mm oak block over a 6 percent moisture swing, so make the movement common-mode or run the grain vertically. The bearing ring that turns relative to the load gets the tight fit; mount bearings in metal housings, not straight into wood.
Lesson complete
Nice work.
Sources for this lesson
- 1Wood Handbook, Chapter 4: Moisture Relations and Physical Properties of Wood. USDA Forest Service, Forest Products Laboratory. 2021. verifiedPublic U.S. government chapter on hygroscopicity, equilibrium moisture content, fiber saturation, shrinkage, swelling, and species data.
- 2Fits and Internal Clearance (ABCs of Bearings). NSK. verifiedA ring that rotates relative to the load direction (a rotating load) needs a tight (interference) fit, or it creeps, slipping around its seat and wearing it; a ring with a stationary load can take a loose fit. For a rotating inner ring with a fixed load direction: tight on the shaft, loose in the housing. Excessive interference can crack the ring; fit choice depends on load, speed, temperature, and the shaft and housing materials.