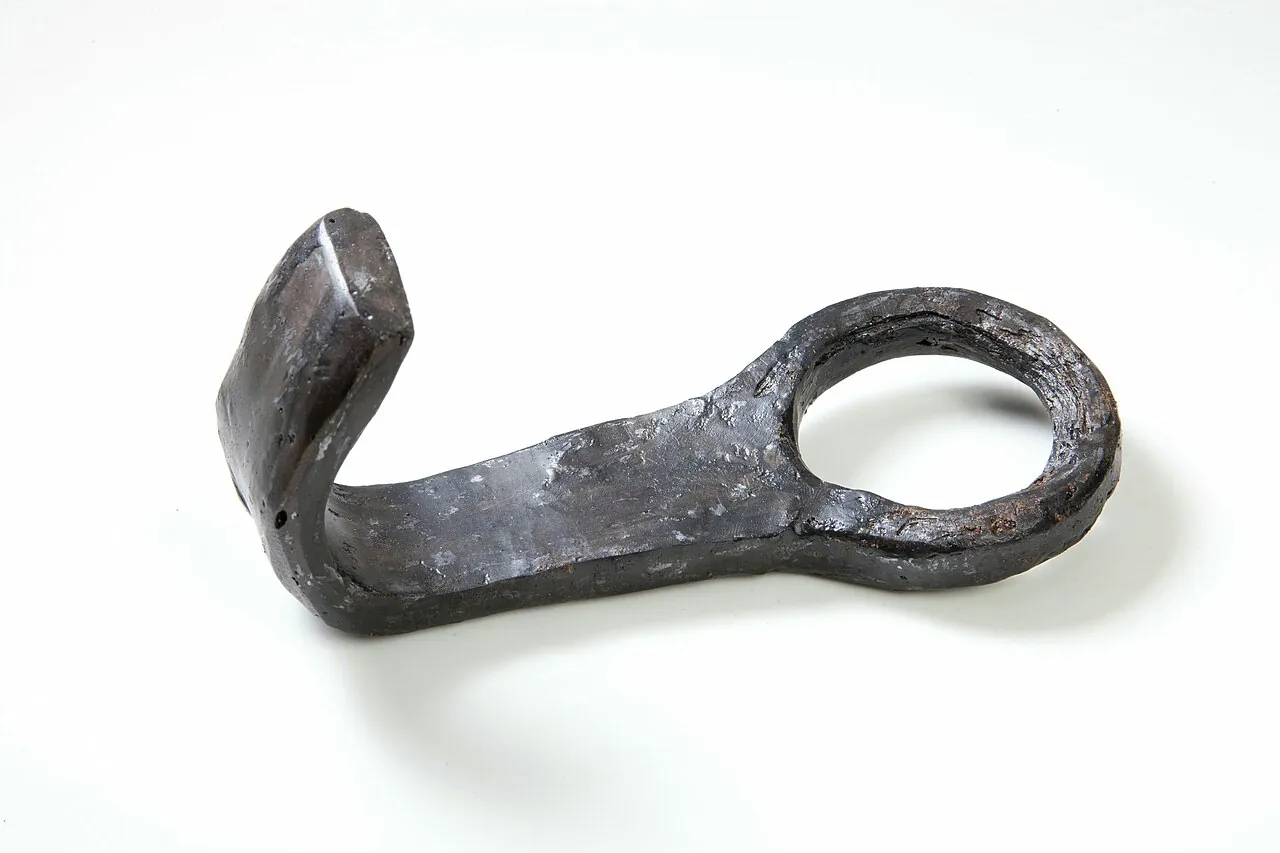
Hooks and S-Hooks
The classic first projects: an S-hook from 1/4-inch round with tapered, scrolled ends, and a wall hook with a flattened, punched mounting tab - covering tapering, scrolling, bending, punching, and finishing with wax.
- 3 min
- 5 steps
- 3 questions
- Lesson 93 of 204
In this lesson
- Why hooks first
- An S-hook
- A wall hook
- Finishing
- What to take from this
Picking up where you left off.
Why hooks first
Hooks use the core skills - tapering, scrolling, bending, punching - in a small, forgiving piece of mild steel that’s useful when done. Trade-school texts start students the same way, with bent and hooked shapes 1.

An S-hook
Stock: 1/4-inch (6 mm) round mild steel, about 6-7 inches (15-18 cm) for a 4-inch hook.
- Taper one end: forge a square taper about 1 inch long at a bright orange, then octagon and round it (see Drawing Out).
- Scroll the tip: curl a tight, small scroll over the anvil edge or with round-nose pliers at heat.
- Repeat on the other end, holding the hot end with tongs.
- First bend: heat one half and bend it over the horn into a C, the scroll facing outward.
- Second bend: heat the other half and bend the opposite way to make the S. Bend at a high heat and only where you want the curve (see Bending and Scrolling) 2.
- True it up: flatten it on the face so it lies in one plane, and adjust the opening.
Optional: give the middle a twist - heat it evenly, clamp one end in the vise, and turn with tongs or a wrench - after squaring that section.
Playback is optional. If the player is unavailable, open the video at its source.
Quick check
Tapers also show off control of the hammer.
A wall hook
Stock: 3/8-inch square, about 8 inches.
- Flatten the mounting end into a tab by drawing it out wide with the hammer face, about 1/8 inch thick.
- Punch two screw holes in the tab at a yellow heat, over the pritchel, and round the tab’s end (see Punching and Drifting).
- Taper the other end to a point and curl a small scroll or a ball.
- Bend the hook up from the tab with a right-angle bend near the top and a curve below.
- Twist a squared section between tab and hook for decoration.
Quick check
Punched holes keep the tab strong around the screw.
Finishing
Wire-brush off scale while the piece is hot. Then, with the steel at about 300-400°F (too hot to touch, not glowing), rub on beeswax or paste wax, or wipe on linseed oil; it smokes, then cures to a durable dark finish. Buff when cool. For outdoors, use paint or a rust-resistant clear finish.
Quick check
Warm steel melts beeswax or paste wax into the surface; it darkens to a nice black.
What to take from this
An S-hook from 1/4-inch round practices tapering, scrolling, and bending: taper and curl both ends, bend one half into a C over the horn, bend the other half the opposite way, and flatten it true. A wall hook adds a flattened, punched tab. Finish mild steel by brushing off scale and rubbing wax or oil onto warm steel.
Lesson complete
Nice work.
Sources for this lesson
- 1Robert H. Harcourt. Elementary Forge Practice. Stanford University Press. 1917. verifiedPublic-domain trade-school text with step-by-step exercises in drawing out, bending, twisting, and welding.
- 2John Lord Bacon. Forge-Practice: Elementary. John Wiley & Sons. 1908. verifiedPublic-domain trade-school text from the Lewis Institute; fire building with coking coal, welding heat and fluxes (sand, borax, sal ammoniac), upsetting, drawing out, bending, punching, and tool-steel hardening and tempering colors (430 F pale yellow to 570 F blue, temper gone near 650 F).